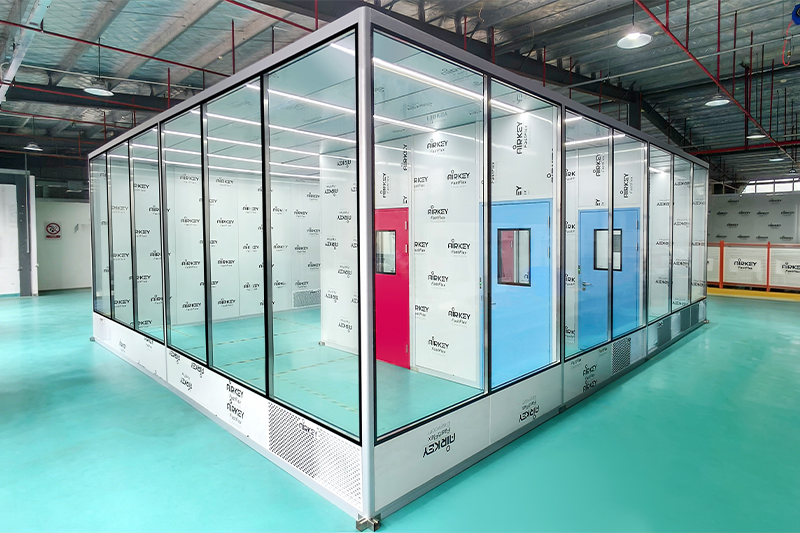
Airkey is a China-based company specialising in modular cleanroom solutions, with 15 years of deep experience in the pharmaceutical industry. In recent years, Airkey has successfully delivered dozens of USP-compliant cleanrooms, primarily for export to the United States, as well as to Panama and Canada. Its projects include standalone USP 797 sterile compounding rooms, standalone USP 800 hazardous drug handling cleanrooms, and complete cleanroom suites that integrate both USP 797 and USP 800 production areas. With a thorough understanding of USP 797 and USP 800 standards, Airkey provides one-stop solutions tailored to each client's specific compliance needs.
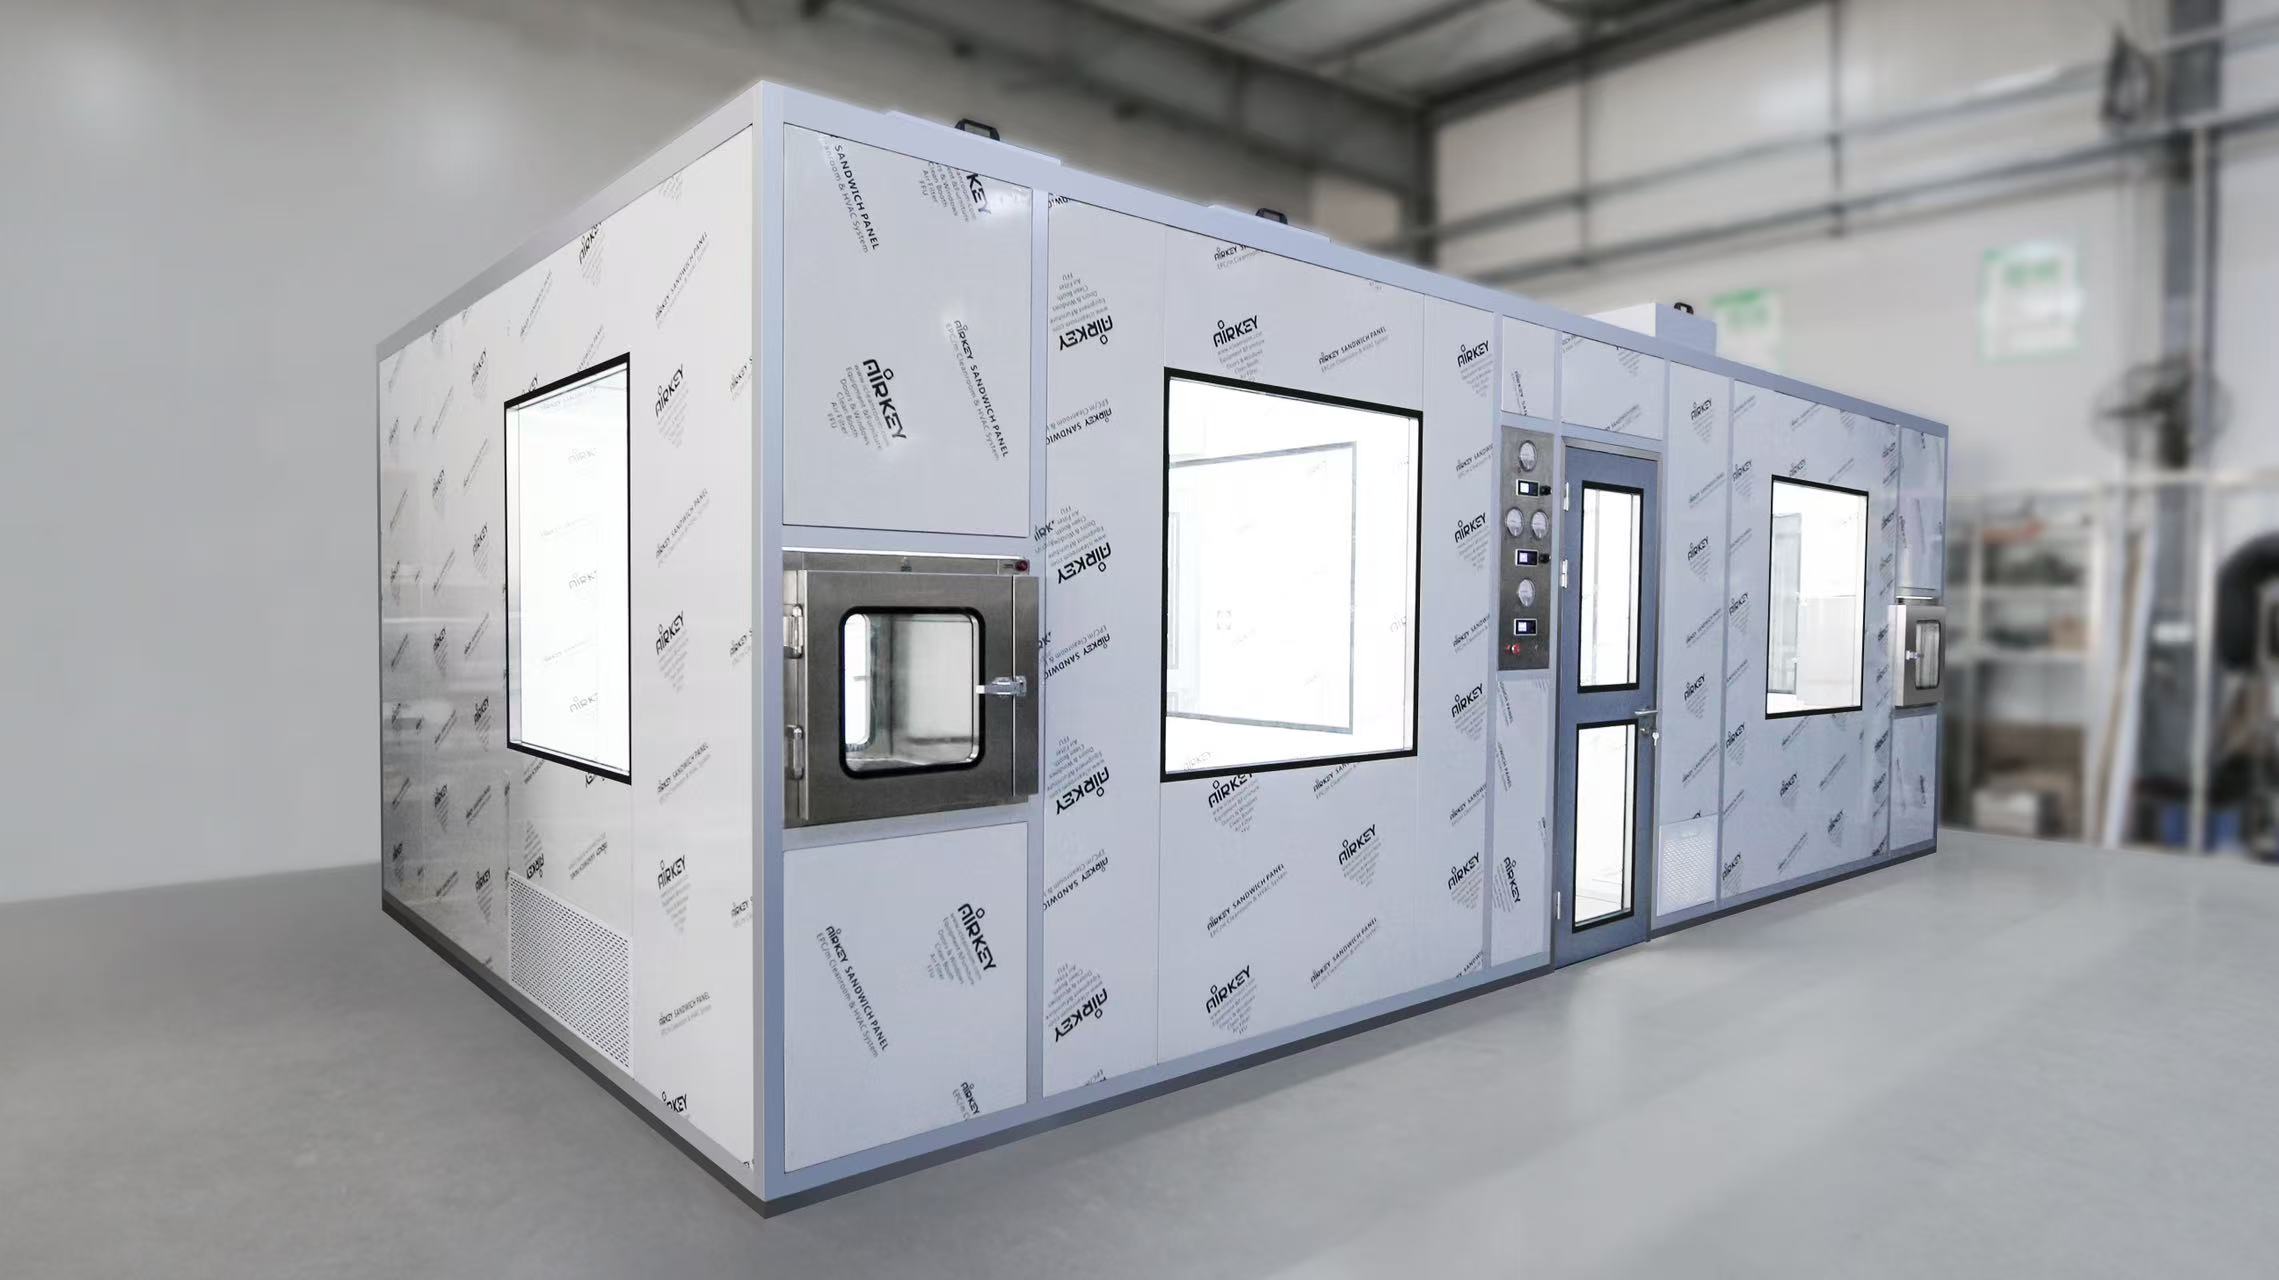
Deep understanding of USP standards
USP 797 and USP 800 impose fundamentally different requirements on cleanroom design and operation. USP 797, which governs sterile compounding, requires a positive-pressure environment to prevent external contamination from entering. USP 800, which governs hazardous drug handling, requires a negative-pressure environment to prevent harmful substances from escaping. This pressure differential is the most critical design decision in any cleanroom facility, and it depends entirely on the core question of "what are we protecting, and what are we protecting against?"
With dozens of USP-compliant cleanroom projects under Airkey's belt, the company has the expertise to precisely design pressure gradients, airflow patterns, and temperature/humidity control systems based on each client's specific application. Whether the requirement is a standalone USP 797 sterile compounding room, a standalone USP 800 hazardous drug handling cleanroom, or a cleanroom suite combining both production areas, Airkey delivers customised solutions that meet the relevant standards.
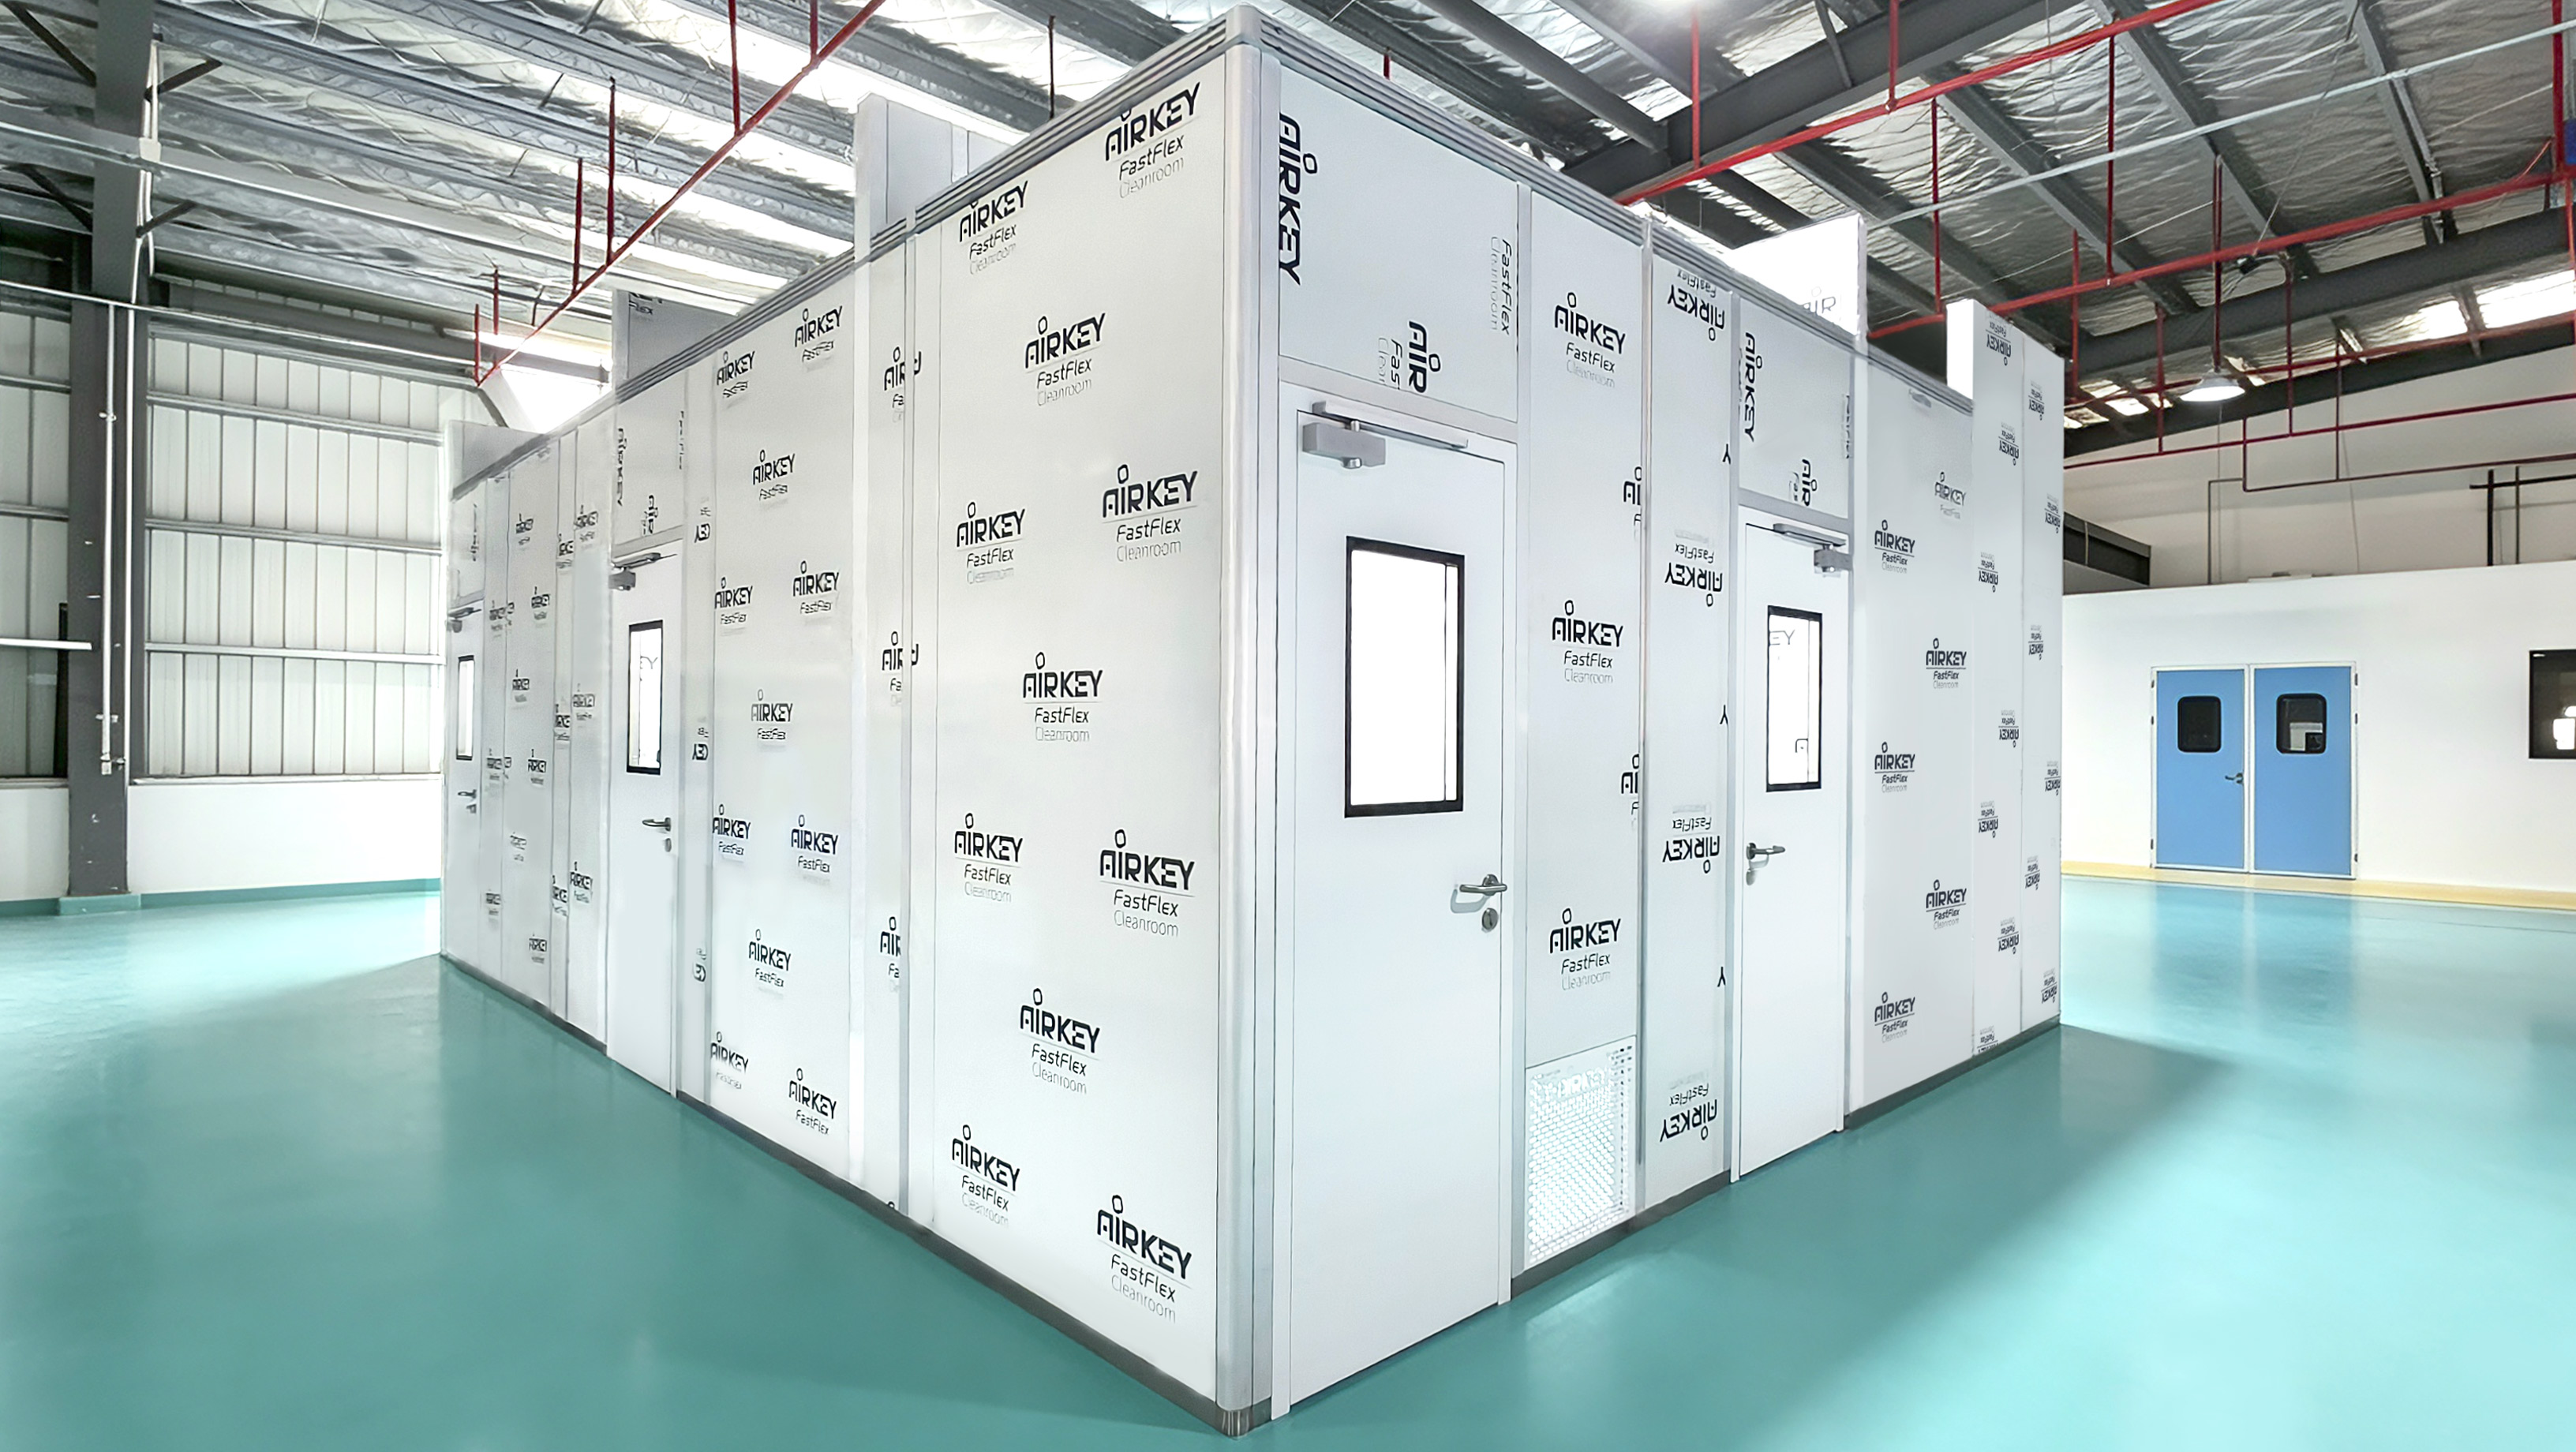
Factory pre-fabrication, pre-assembly, and testing: Ensuring quality and efficiency
Airkey employs a "Factory-Proven" delivery model, which is fundamentally different from the approach of most suppliers in the industry who provide only components and instructions.
Complete pre-assembly and electrical integration
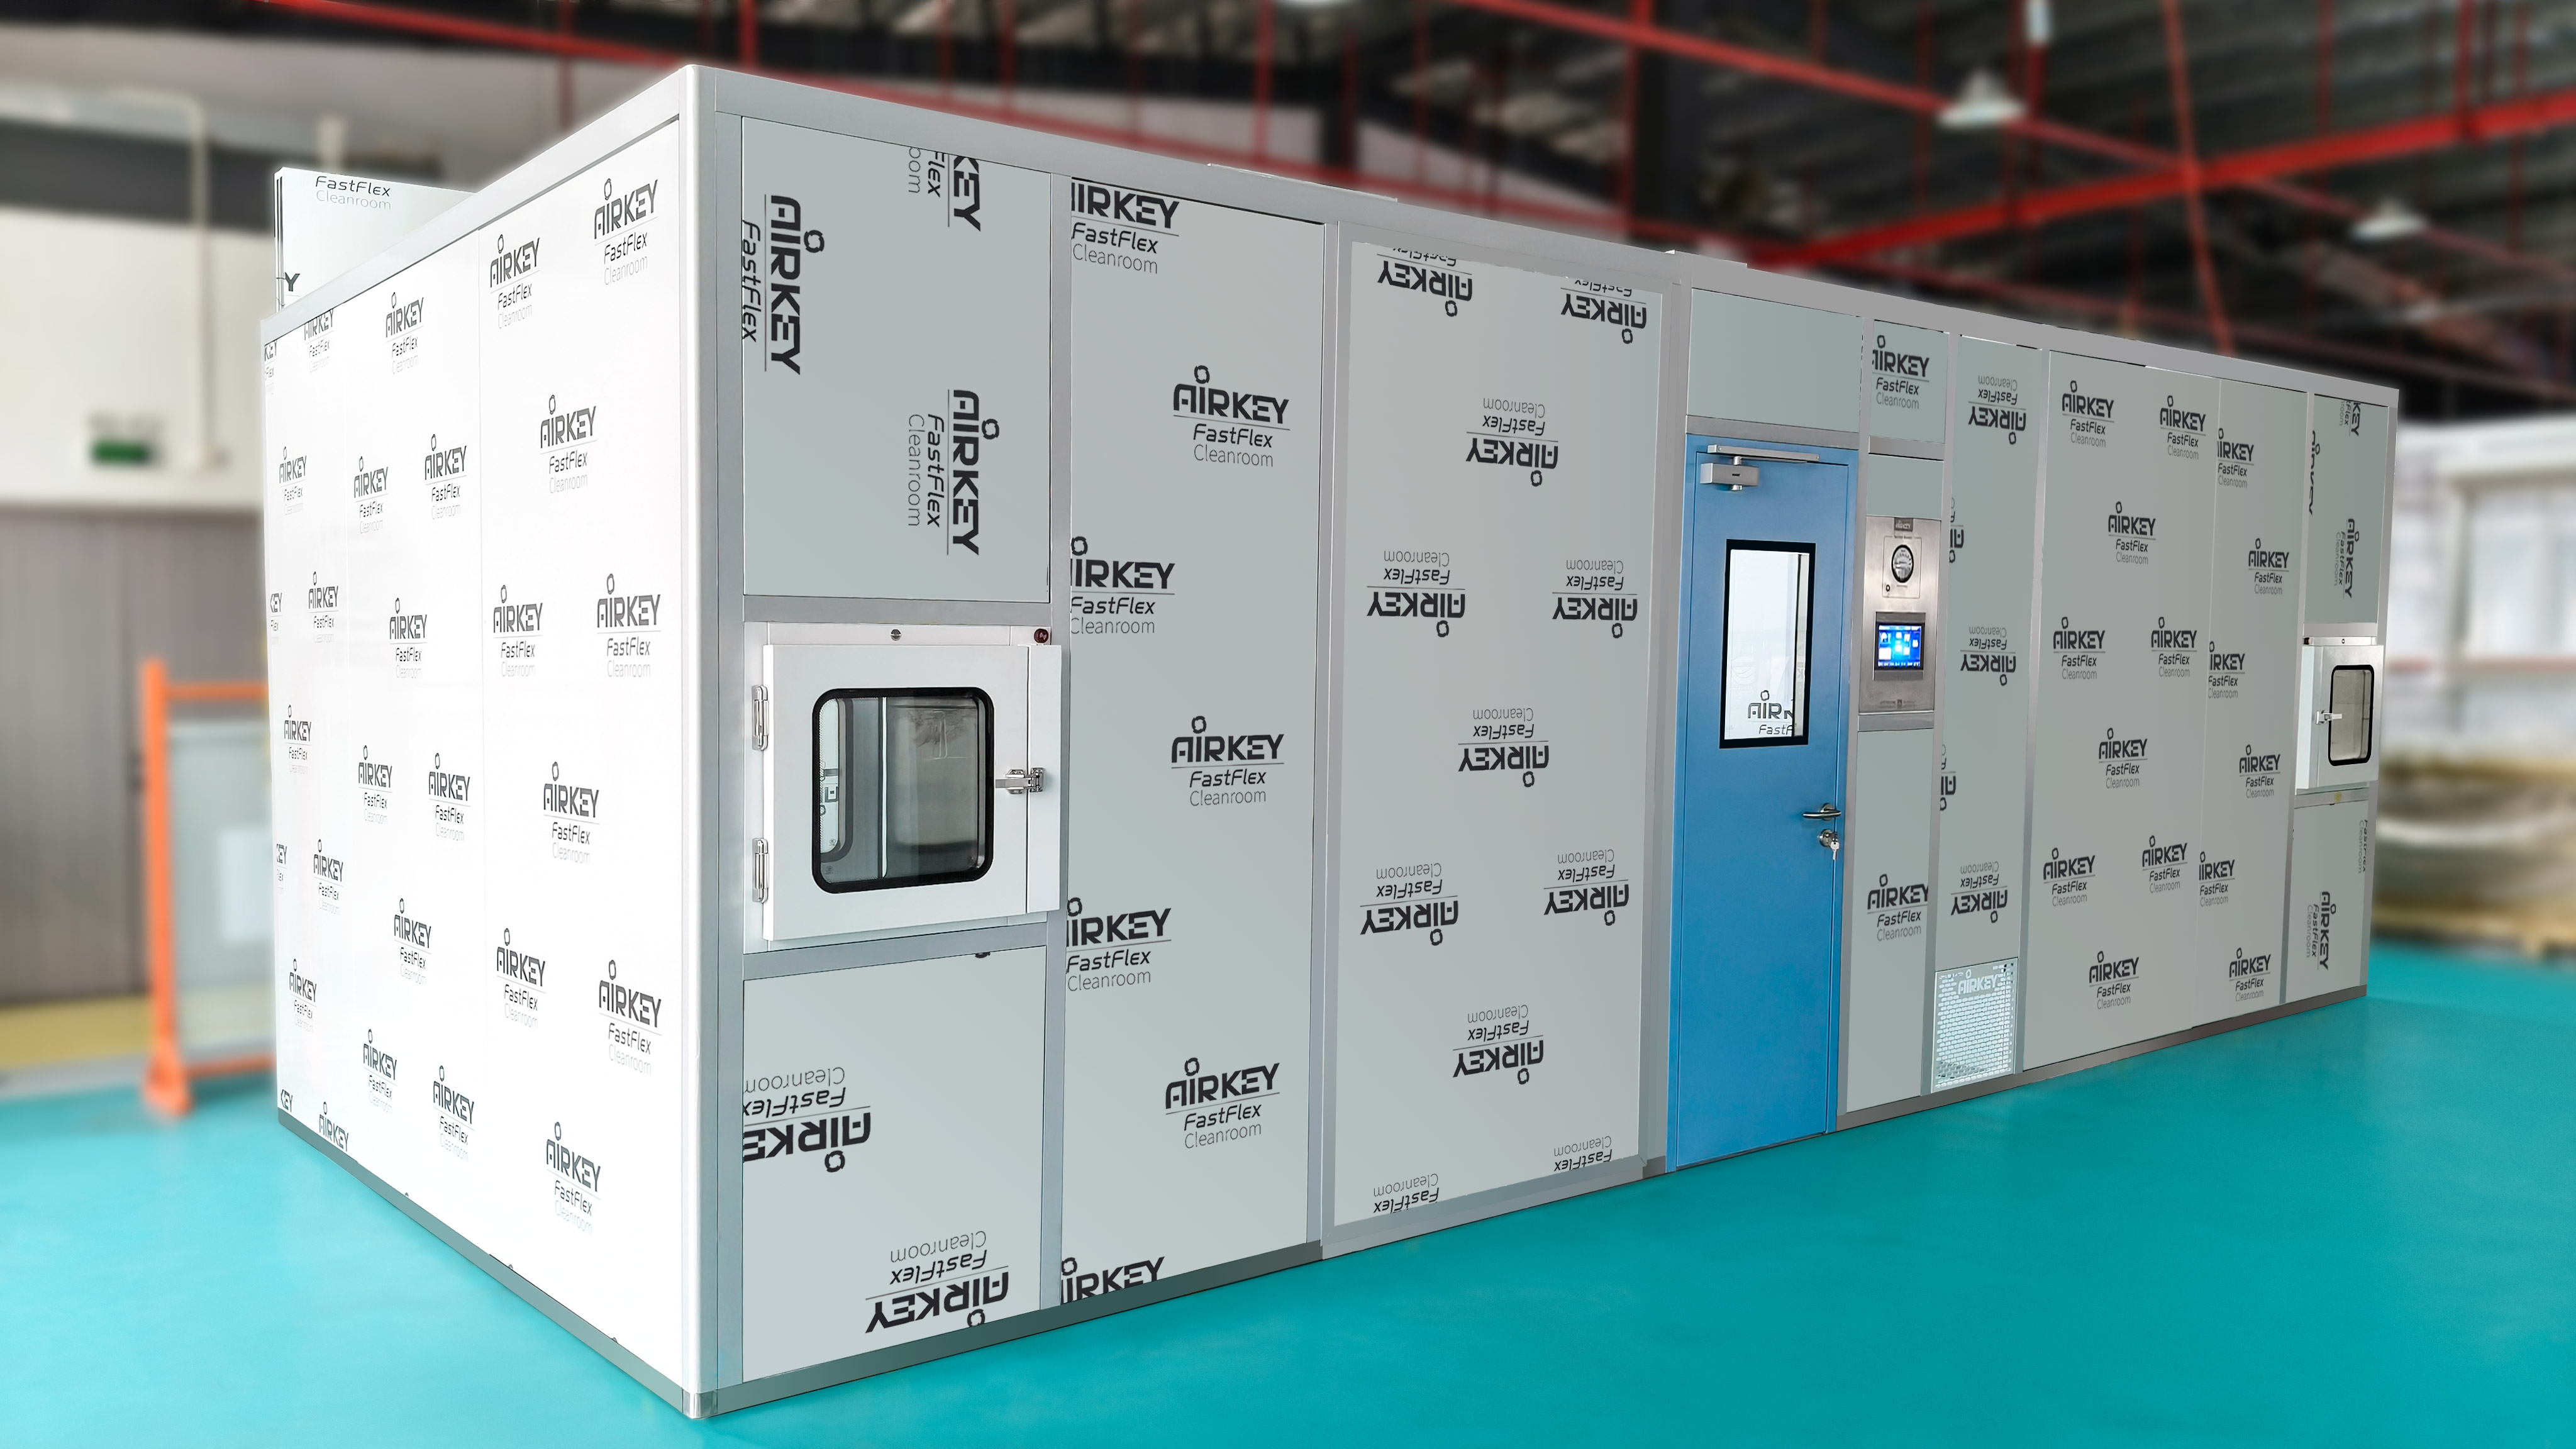
Every cleanroom undergoes full mechanical assembly before shipment, including the installation of walls, ceilings, doors, pass-through windows, and return air columns, as well as the electrical integration and live testing of lighting, controls, and FFU wiring. This means that what the client receives on site is not a "kit" to be assembled, but a complete cleanroom that has already been operated and tested as a fully integrated system.
Rigorous performance verification
During the factory testing phase, Airkey uses calibrated instruments from internationally recognised brands to conduct comprehensive performance verification of the cleanroom, including measurements of airflow uniformity, pressure differential, illuminance, noise level, and particle counting. All test results are documented to ensure compliance with ISO 14644-1 standards.
On-site installation becomes connection
Because the cleanroom has already been pre-assembled and tested at the factory, on-site installation shifts from "construction" to "connection," significantly reducing installation time while eliminating the performance risks associated with on-site assembly.
Pharmaceutical project experience
Airkey has extensive project experience in the pharmaceutical cleanroom sector. Recent representative projects include:
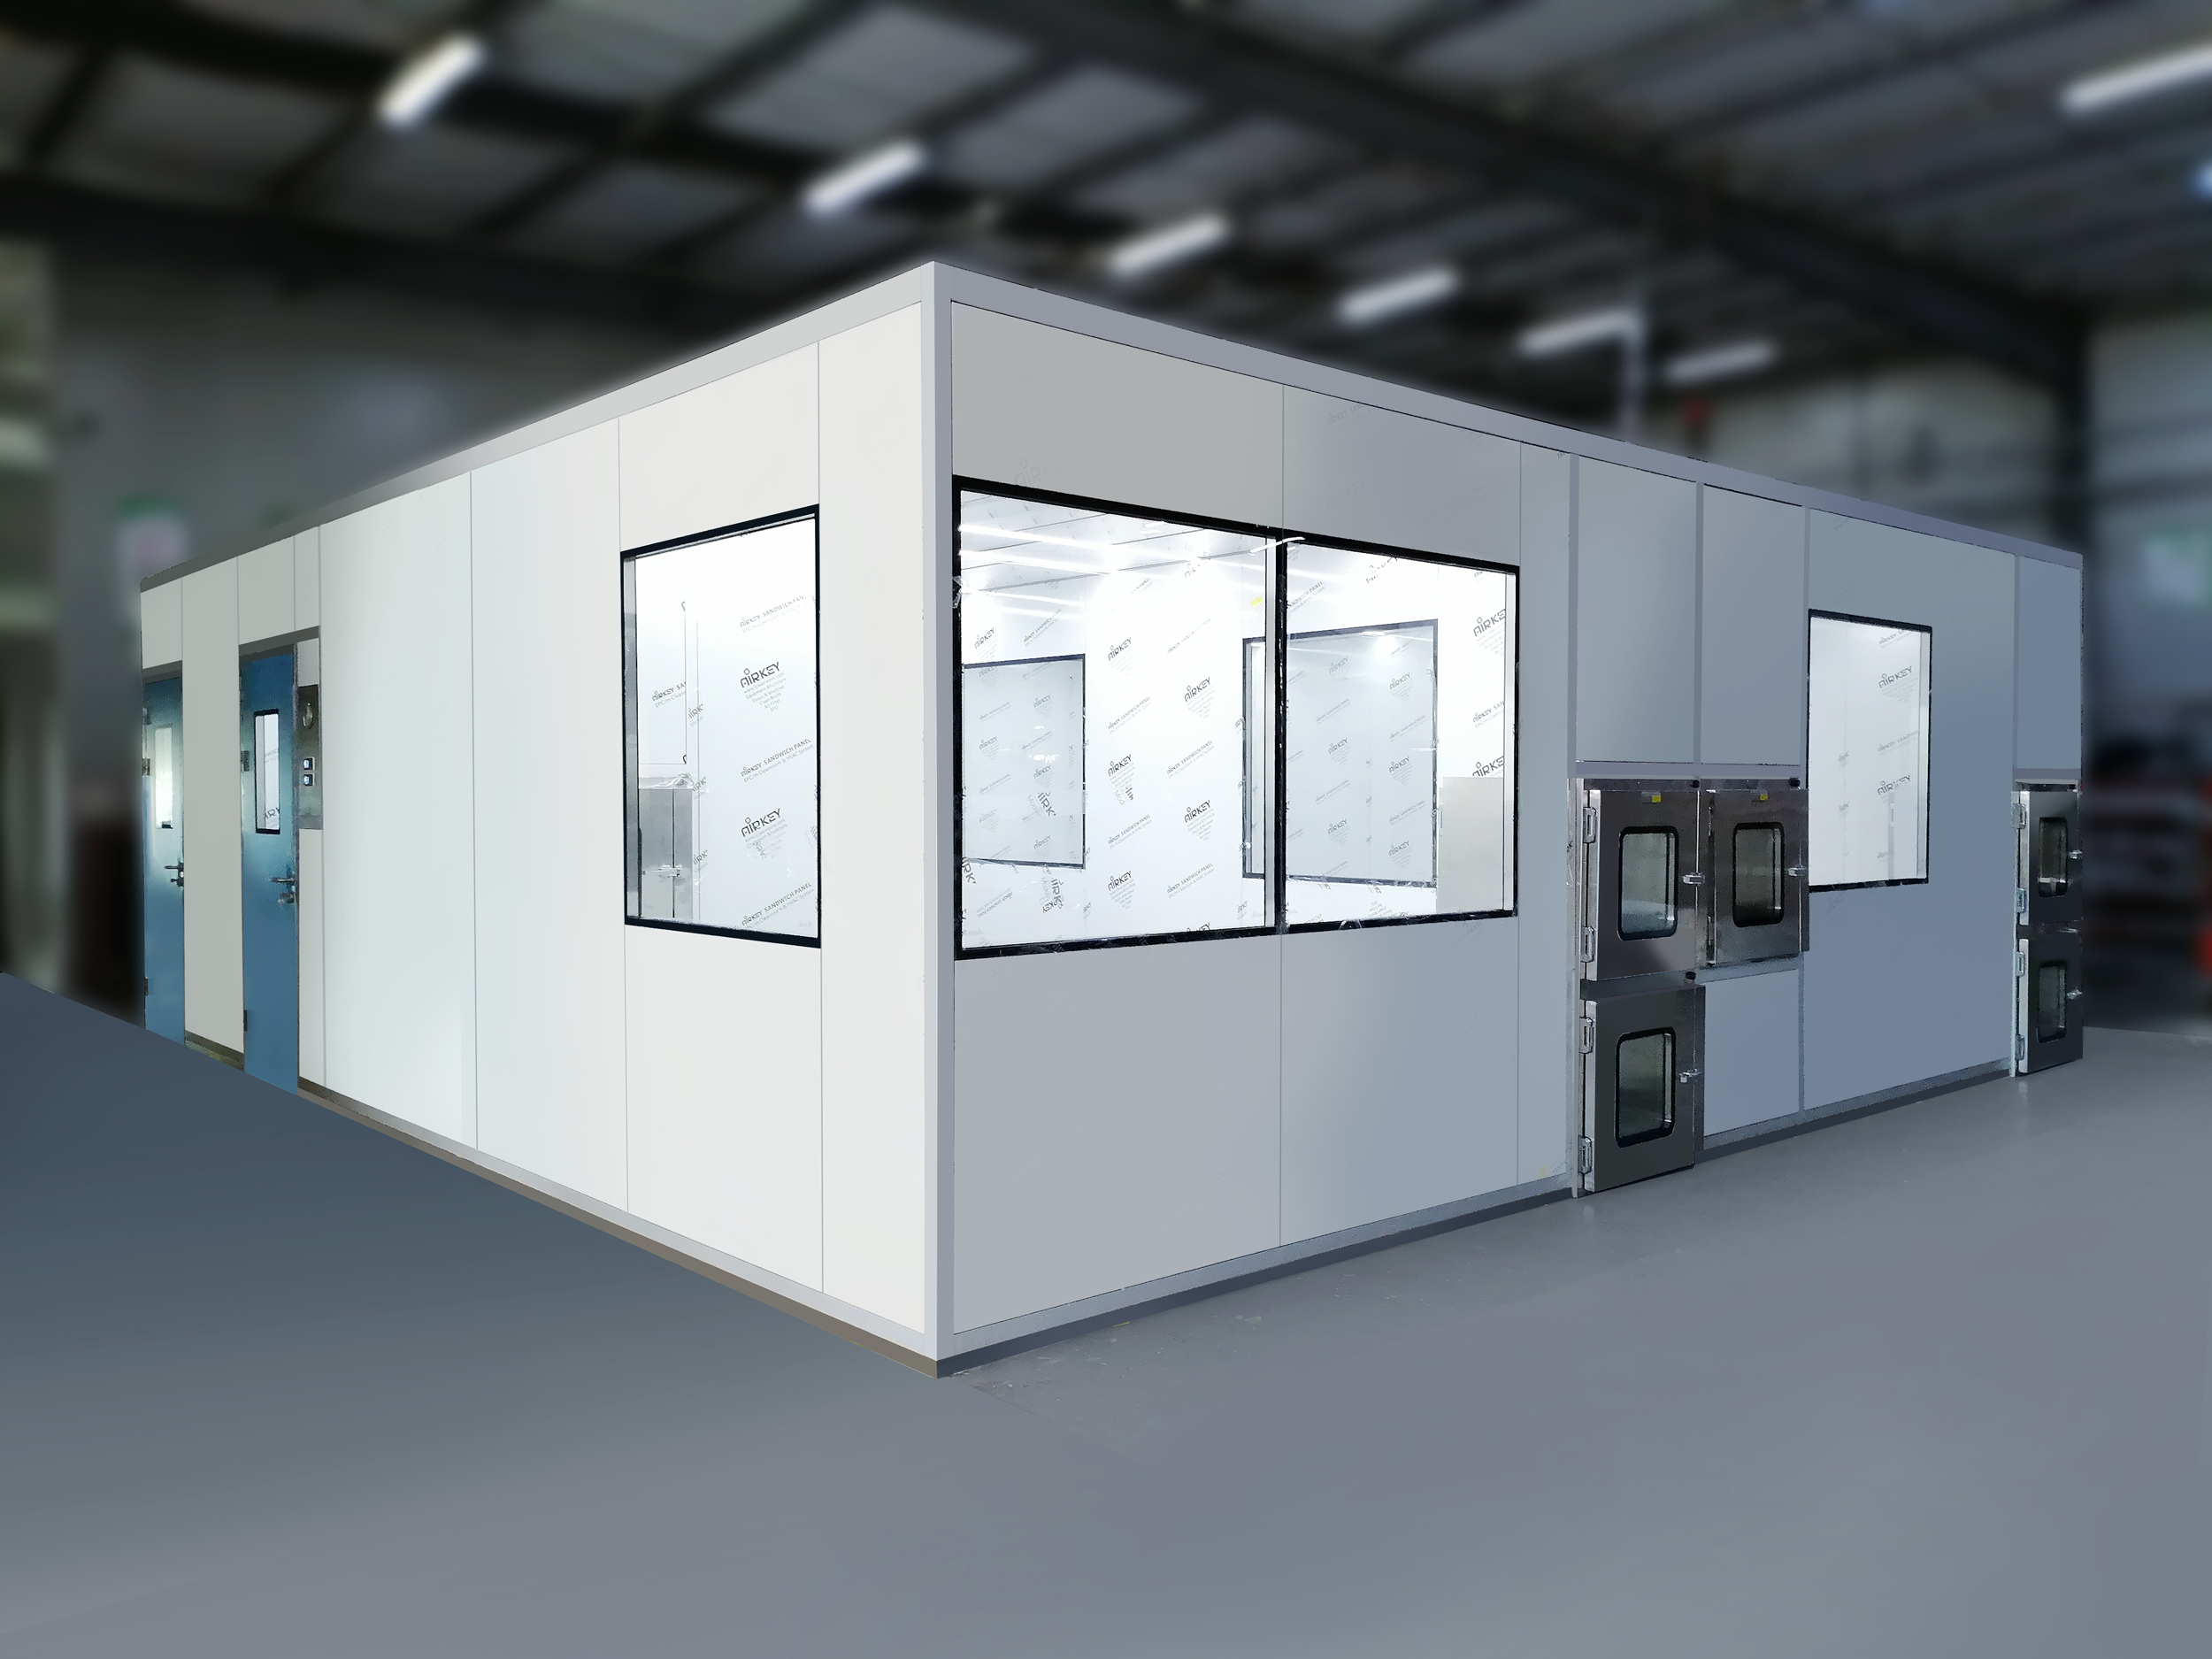
- U.S. Pharmaceutical Client Project 1: 8.5m × 3m × 2.8m, ISO 7, compliant with USP 797/800, equipped with automatic sensor sliding doors, pass-through windows, and pre-wired U.S. standard outlets
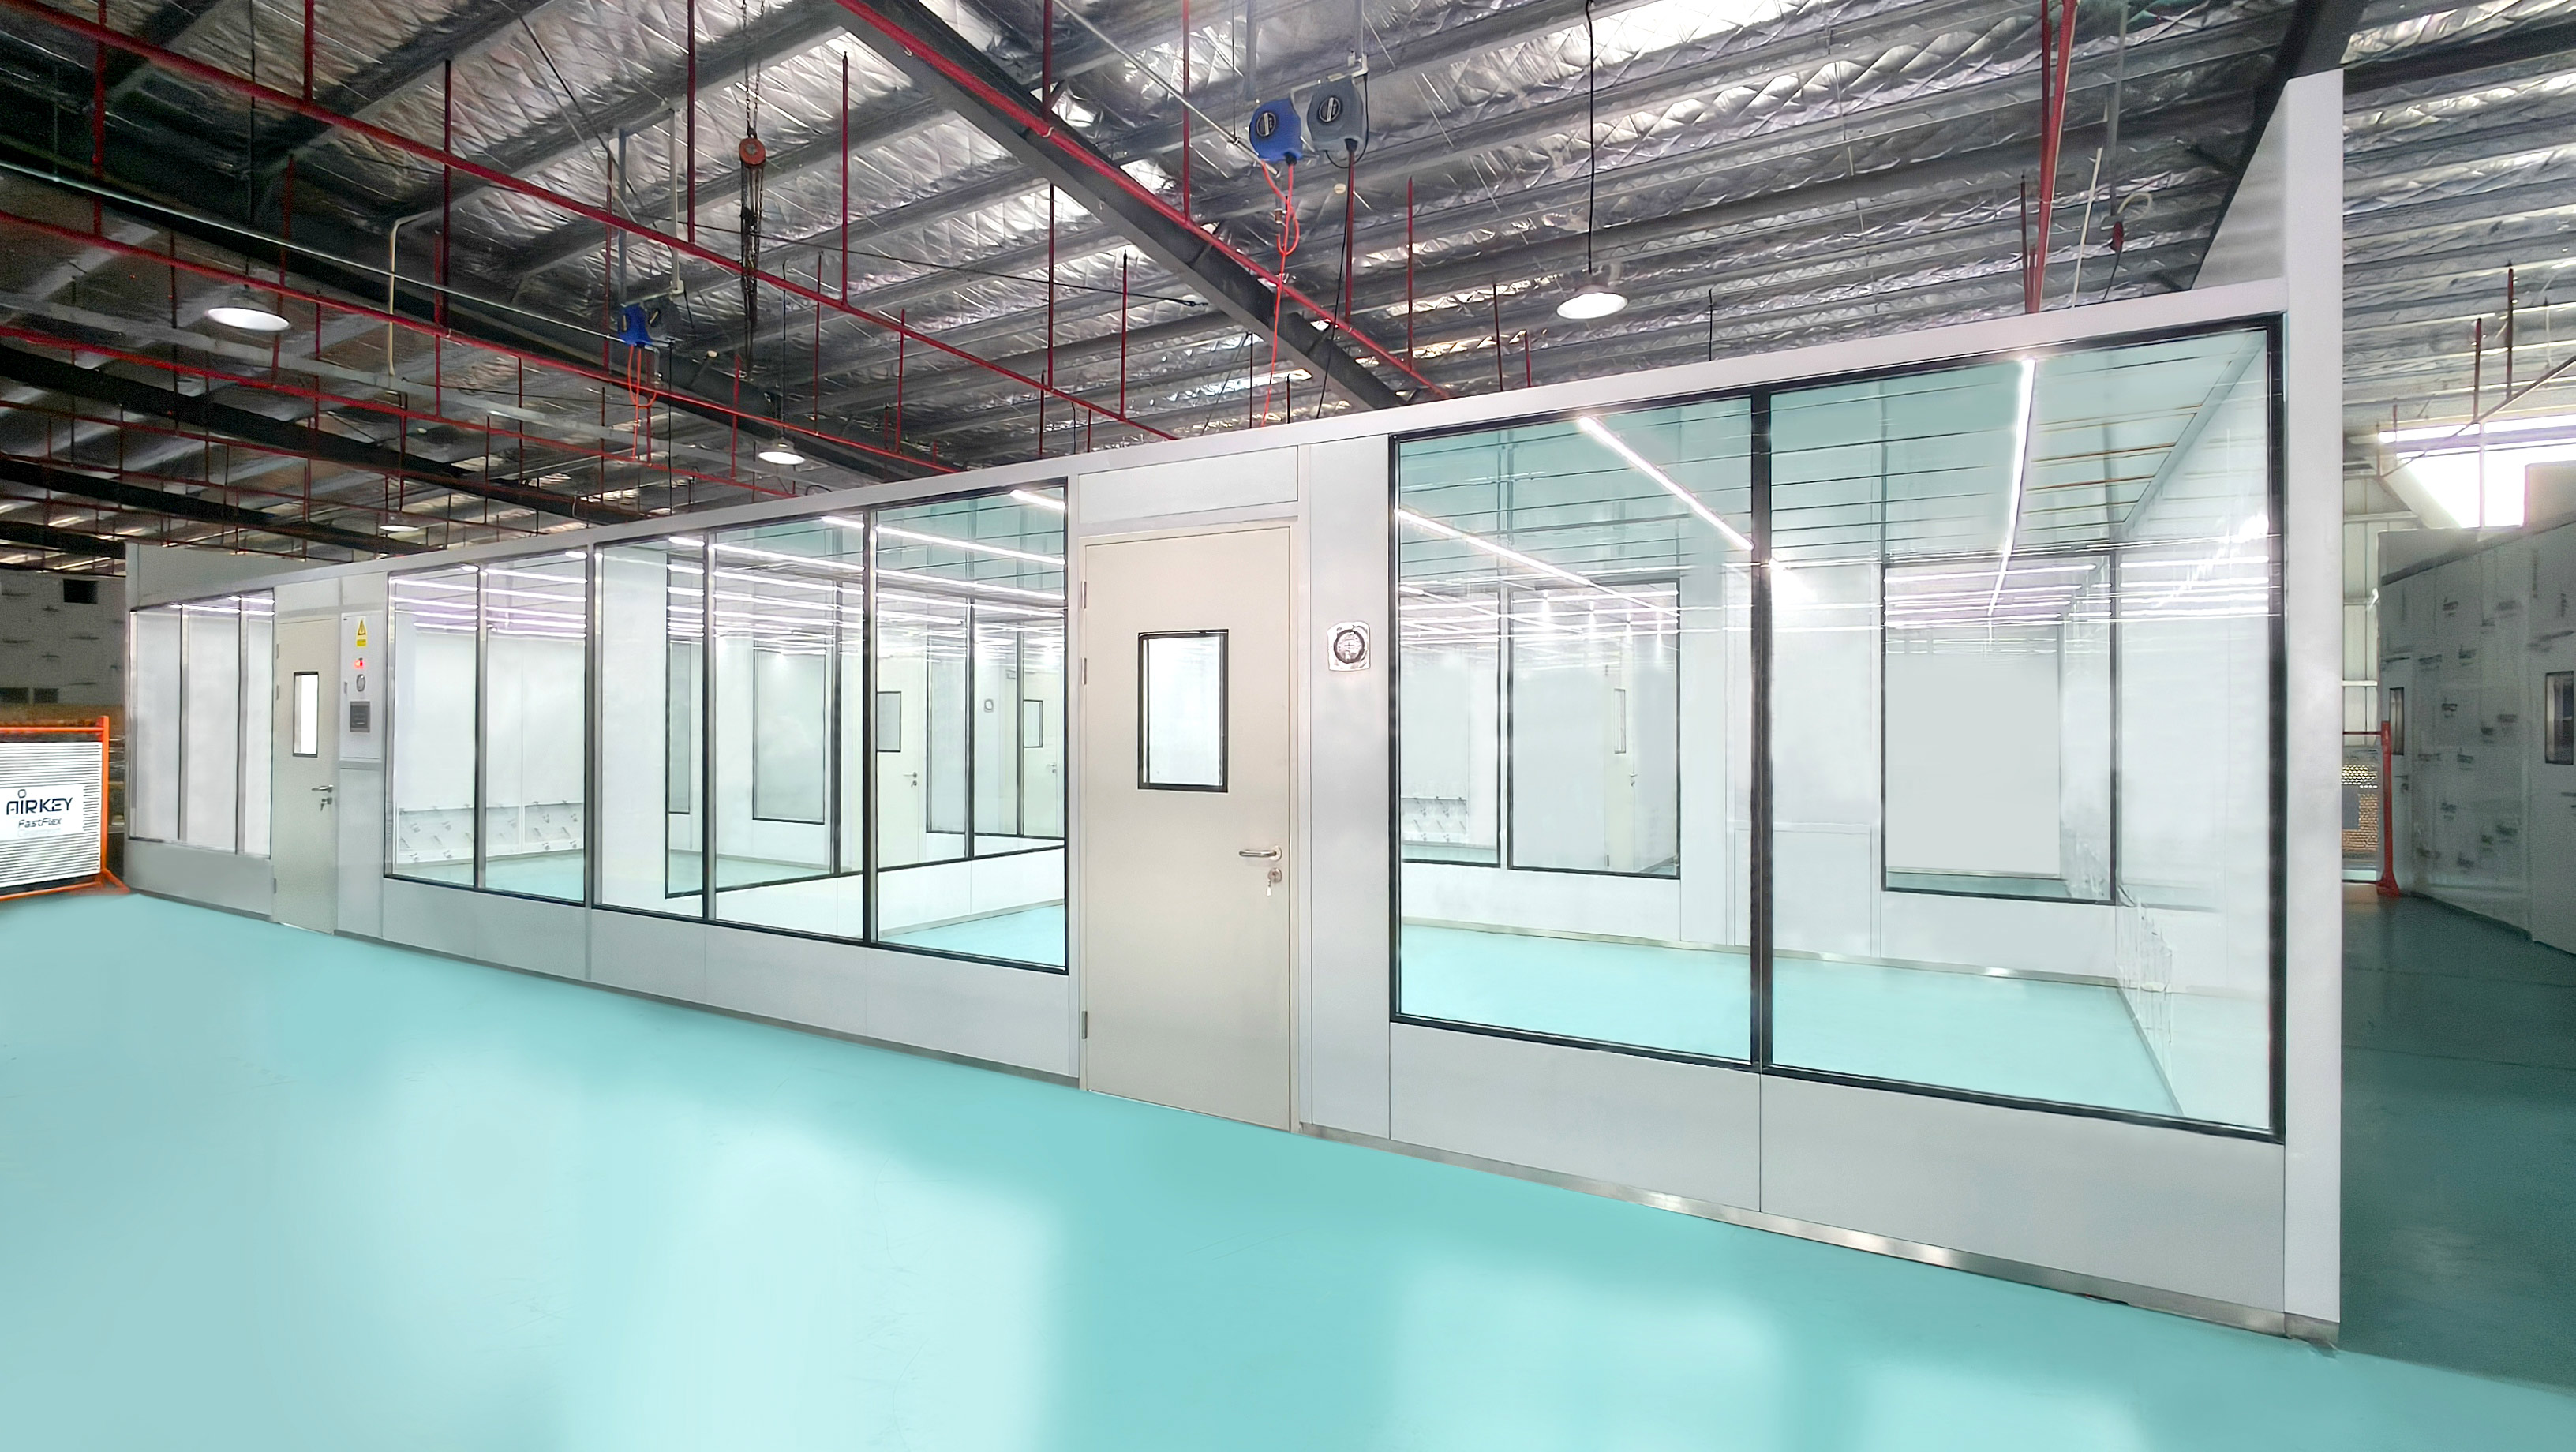
- U.S. Pharmaceutical Client Project 2: 7.3m × 4.8m × 3m, ISO 7, comprising 5 independent rooms, each pre-installed with tempered glass doors, pass-through windows, and dedicated return air columns
- Canada Pharmaceutical Project: 6.2m × 3.1m × 2.4m, ISO 8, comprising a gowning room, main cleanroom, and pass-through window
Why choose Airkey
- 15 years of deep roots in the pharmaceutical industry: A thorough understanding of pharmaceutical regulatory requirements and client needs
- Dozens of USP-compliant projects: Covering USP 797, USP 800, and combined cleanroom suites
- Factory-proven delivery model: Pre-assembly and pre-testing ensure certainty in performance and quality
- Rich export experience: Products exported to the United States, Canada, Panama, and other markets
- Customisation capability: Personalised solutions based on each client's specific application and site conditions
Airkey is committed to providing high-quality, compliant, and reliable modular cleanroom solutions to pharmaceutical clients worldwide. Whether for a new project or an expansion, the company is ready to provide professional support and service.